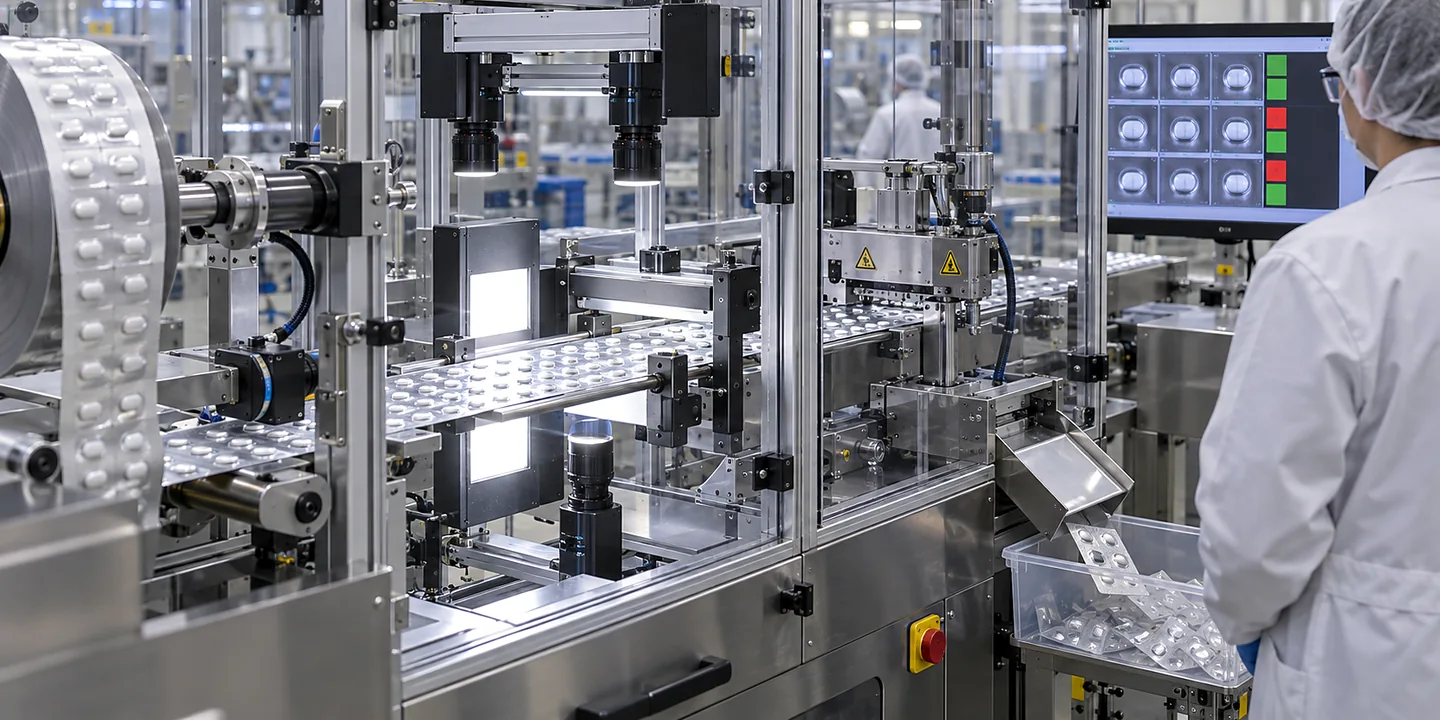
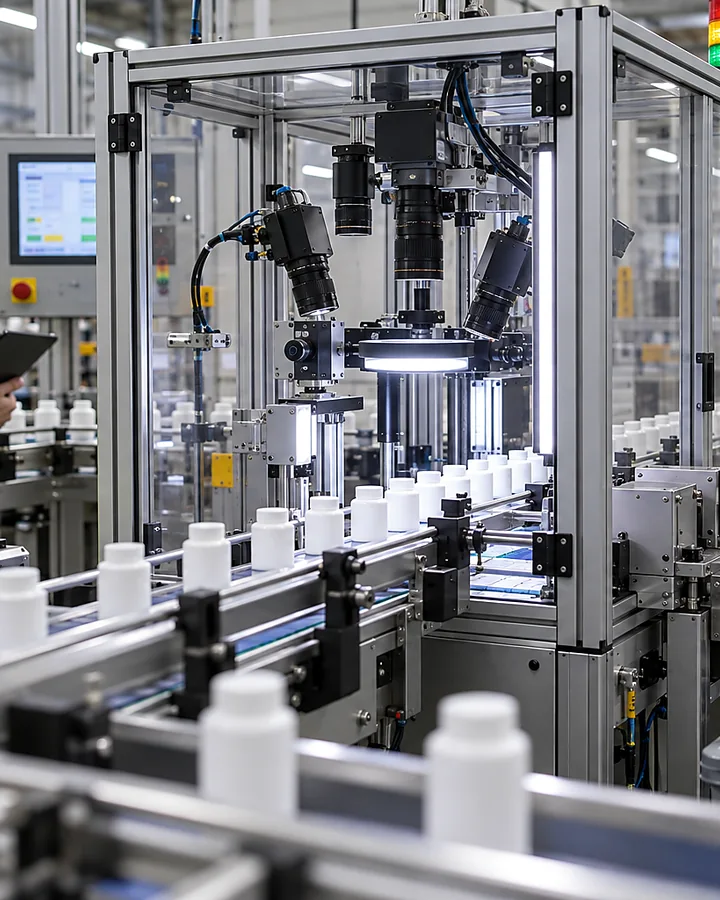
Define the visible assembly defect or measurement that the camera must judge before selecting medical-device vision equipment. Trial good, bad and marginal production samples under the intended presentation and lighting, then agree challenge and reject criteria. Optical feasibility does not establish clinical function or replace the manufacturer's product-validation and release responsibilities.
Speak directly with Oxford Vision Systems about medical-device assembly visual checks.
Quick answer
How should we define and validate the scope of a medical-device vision inspection?
Turn the product requirements into specific visible inspection decisions, with approved samples and acceptance limits. Include expected manufacturing variation and marginal defects in the challenge set. Agree documentation, recipe control and validation responsibilities with the manufacturer’s quality team, while recording requirements that cannot be established by the demonstrated optical method.
Application decisions
Translate device assembly requirements into visible checks
The inspection brief should name the observable feature and the decision required. Optical checks can support a manufacturer’s production controls, while device function and product release need their own defined evidence.
Decision 1
Write an observable acceptance decision
Replace a broad requirement such as inspect the device with separate checks for a visible component, orientation, gap, mark or assembly feature. Identify the view and acceptance boundary for each one. The manufacturer’s quality team should approve what constitutes an acceptable, defective and uncertain result. Avoid claiming detection of a hidden feature from an unrelated visible proxy.
Decision 2
Build an approved sample challenge set
Include normal variation, known defects and examples close to the acceptance boundary. Record the origin and approved classification of each sample so trial results are reviewable. A collection used to adjust the inspection is not automatically independent evidence of its performance. Agree how additional challenge samples are selected and retained under the manufacturer’s own quality procedures.
Decision 3
Account for fixture and material variation
Trial the permitted part movement in its production nest and the actual range of surface colour, texture or translucency. Fixture wear, glare and obscured features can alter the image even when the assembly is unchanged. State the proposed inspection stage so components fitted later do not hide the feature being assessed. Record the optical coverage and remaining blind areas.
Decision 4
Define recipe and change control
Associate the approved inspection recipe with the correct device variant. Identify who can change limits, images, programmes or access permissions and which changes require review. Challenge an incorrect recipe and an absent product identity. Keeping the settings controlled makes repeat results interpretable; it does not replace the manufacturer’s validation responsibilities or establish regulatory conformity on its own.
Decision 5
Include reject and missing-result scenarios
Follow each result to the correct device or carrier. Specify what happens when no image is captured, processing fails or rejection is not confirmed. Challenge stop and restart conditions and any manual removal of parts. Where records are required, define the link between the device or batch, recipe version, result and disposition without assuming every installation needs the same retention design.
Decision 6
Separate optical evidence from product claims
Report the samples, setup, challenge conditions, false accepts, false rejects and exclusions agreed for the trial. The responsible manufacturer decides the validation and release requirements for its product and process. A camera showing correct visible assembly does not establish sterility, material identity, bond strength or clinical function. Include separate checks where those properties are part of the requirement.
Two useful starting points for medical device vision inspection
The right choice changes with visible defect or measurement definition for medical-device assembly visual checks, good, bad and marginal sample range, your line layout and required results.
Your route from an initial enquiry to a working solution
You can review decisions about recipe, reject and line-control interfaces and false-accept, false-reject and challenge criteria at each stage.
01
Define the Visible Decision and Collect Representative Samples
Share representative good, bad and marginal samples, including the normal range for visible defect or measurement definition for medical-device assembly visual checks and the difficult good, bad and marginal sample range cases.
02
Prove Contrast, Presentation and Timing in an Optical Trial
Compare suitable methods and use focused trials to show how each option performs against part presentation and production speed.
03
Integrate Cameras, Controls, Reject Handling and Recipes
Connect the equipment to your line, services and controls while resolving optics, lighting and environmental conditions for day-to-day operation.
04
Challenge Marginal Cases and Document Agreed Results
Confirm recipe, reject and line-control interfaces, then complete and record false-accept, false-reject and challenge criteria before your operating team takes over.
Important limits
Know what needs a separate check
Regulated-product validation and release decisions remain with the responsible manufacturer.
A camera can only assess a property made visible and repeatable by the inspection setup.
Sample diversity and marginal cases determine how meaningful a feasibility result is.
Your final solution for medical-device assembly visual checks must reflect the law, current standards and site-specific risks that apply to your installation.